Zinc Electroplating - Overview
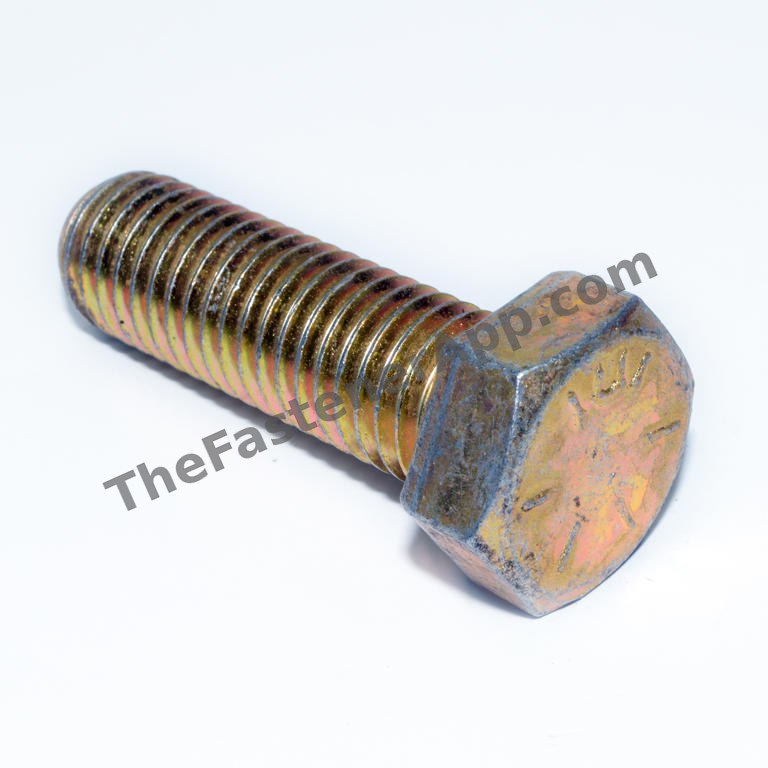
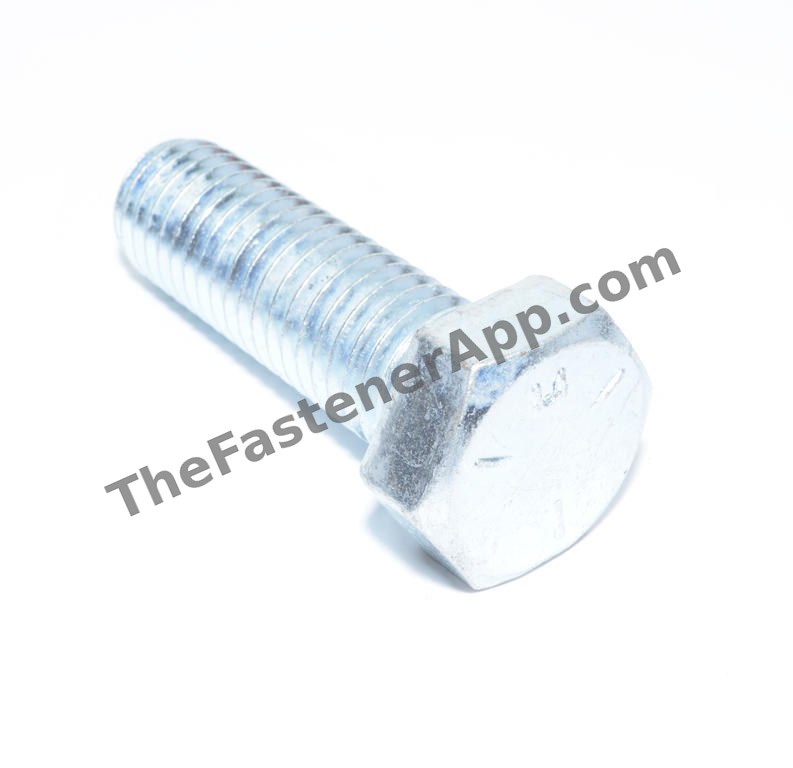
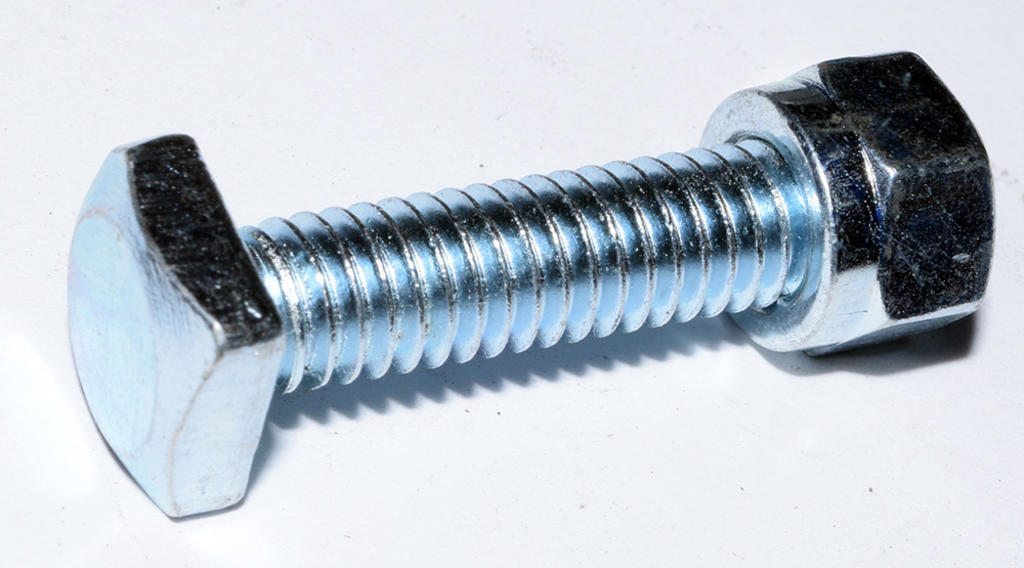
Zinc electroplating deposits a thin layer of zinc that corrodes first to protect the steel. A chromate or passivate on top gives the color and adds corrosion resistance.
ASTM B633 service condition (zinc thickness)
| Service condition | Designation | Minimum zinc |
|---|---|---|
| SC 1 - mild (indoor, dry) | Fe/Zn 5 | 5 micrometres |
| SC 2 - moderate (indoor, some moisture) | Fe/Zn 8 | 8 micrometres |
| SC 3 - severe (outdoor, wet) | Fe/Zn 12 | 12 micrometres |
| SC 4 - very severe | Fe/Zn 25 | 25 micrometres |
Threaded fasteners are usually limited to about 8 - 12 micrometres so they still assemble. ASTM F1941 covers electrodeposited coatings specifically for fasteners.
ASTM B633 finish types
| Type | Finish |
|---|---|
| I | Zinc as plated, no supplementary treatment |
| II | Colored chromate (yellow, olive drab, black) - hexavalent |
| III | Colorless chromate (clear) - hexavalent |
| IV | Phosphate |
| V | Colorless passivate - trivalent |
| VI | Colored passivate - trivalent |
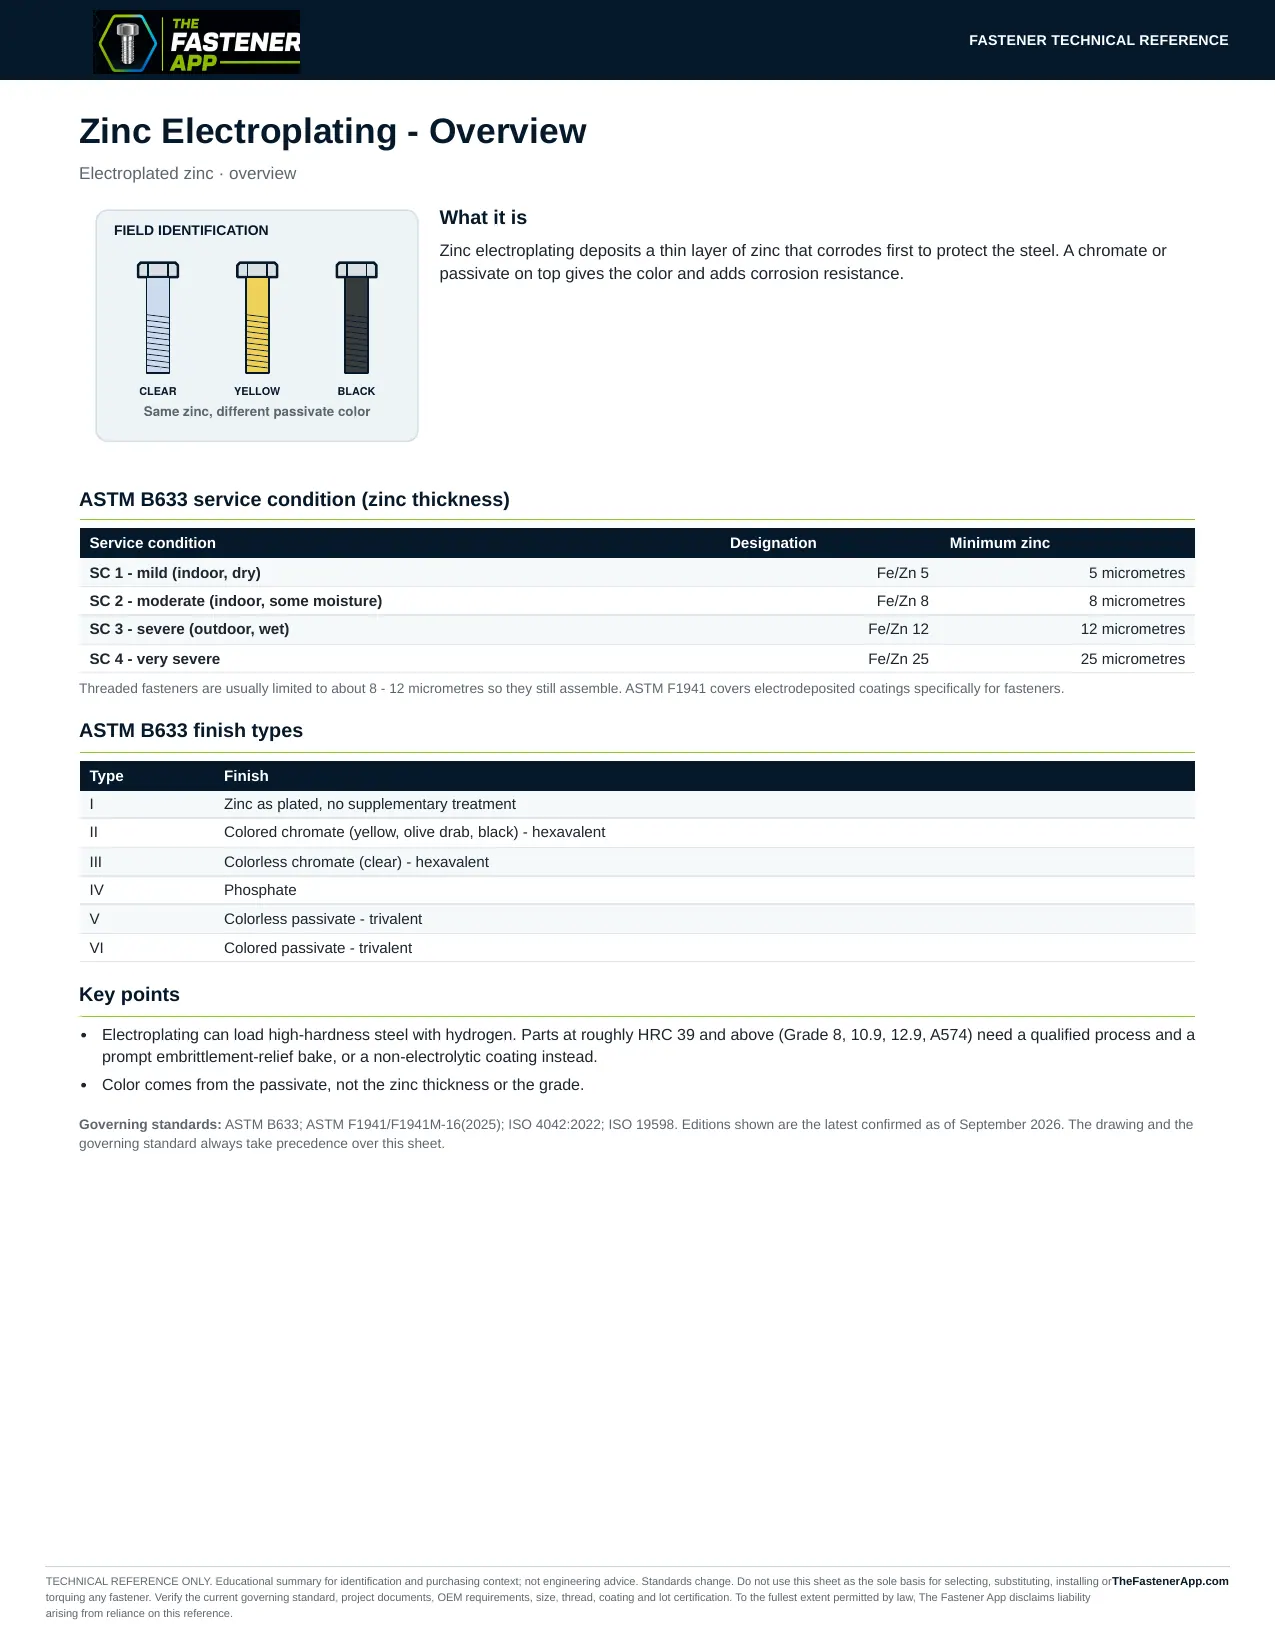
These tables carry the same figures as the printed sheet below.
The printed sheet
See an error on this sheet?
Tell us what is wrong.
Text version of this sheet
Electroplated zinc · overview
What it is
FIELD IDENTIFICATION
Zinc electroplating deposits a thin layer of zinc that corrodes first to protect the steel. A chromate or
passivate on top gives the color and adds corrosion resistance.
CLEAR
YELLOW
BLACK
Same zinc, different passivate color
ASTM B633 service condition (zinc thickness)
Service condition
Designation
Minimum zinc
SC 1 - mild (indoor, dry)
Fe/Zn 5
5 micrometres
SC 2 - moderate (indoor, some moisture)
Fe/Zn 8
8 micrometres
SC 3 - severe (outdoor, wet)
Fe/Zn 12
12 micrometres
SC 4 - very severe
Fe/Zn 25
25 micrometres
Threaded fasteners are usually limited to about 8 - 12 micrometres so they still assemble. ASTM F1941 covers electrodeposited coatings specifically for fasteners.
ASTM B633 finish types
Type
Finish
I
Zinc as plated, no supplementary treatment
II
Colored chromate (yellow, olive drab, black) - hexavalent
III
Colorless chromate (clear) - hexavalent
IV
Phosphate
V
Colorless passivate - trivalent
VI
Colored passivate - trivalent
Key points
Electroplating can load high-hardness steel with hydrogen. Parts at roughly HRC 39 and above (Grade 8, 10.9, 12.9, A574) need a qualified process and a
prompt embrittlement-relief bake, or a non-electrolytic coating instead.
Color comes from the passivate, not the zinc thickness or the grade.
Governing standards: ASTM B633; ASTM F1941/F1941M-16(2025); ISO 4042:2022; ISO 19598. Editions shown are the latest confirmed as of September 2026. The drawing and the
governing standard always take precedence over this sheet.
torquing any fastener. Verify the current governing standard, project documents, OEM requirements, size, thread, coating and lot certification. To the fullest extent permitted by law, The Fastener App disclaims liability
arising from reliance on this reference.
Fastener Guide reference FG-BBA6B5 · thefastenerapp.com/fastener-guide/plating-coatings-finishes/zinc-electroplating-overview · © The Fastener App. Reference only — verify the current governing standard, drawing and manufacturer data before specifying or installing.