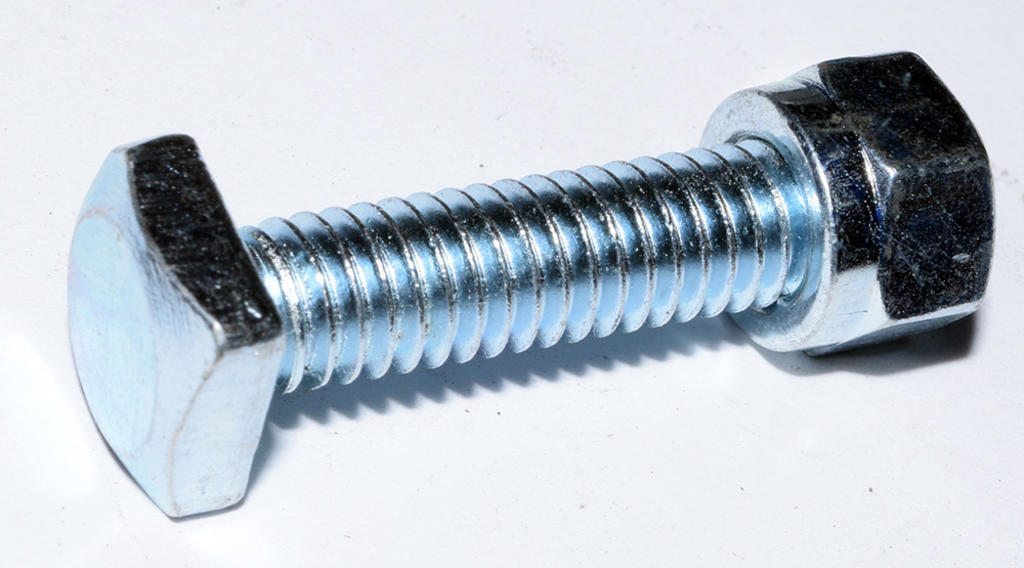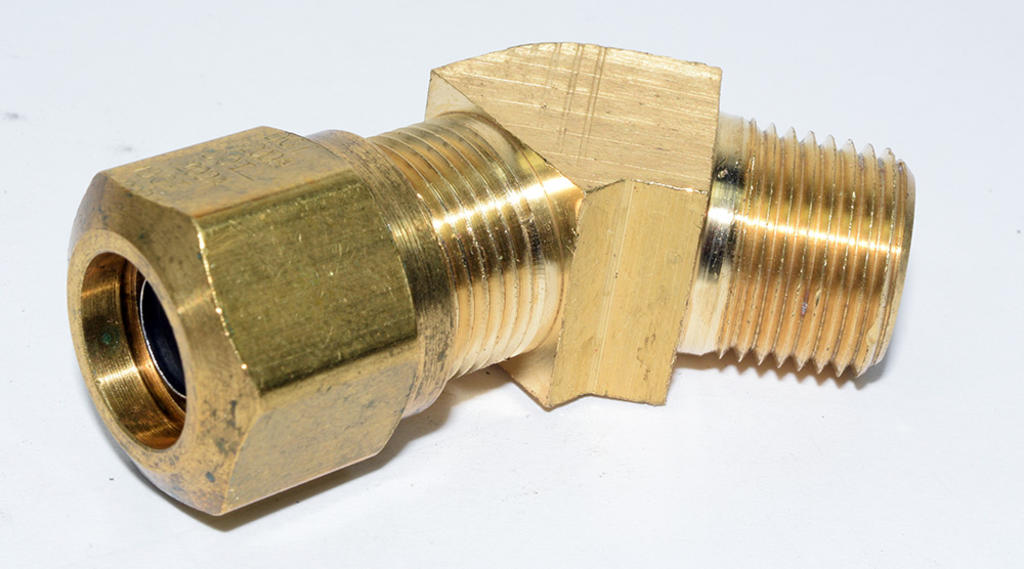
How to Identify Thread Diameter & Pitch
A complete thread identification needs diameter plus pitch/TPI and thread series/form.
See an error on this sheet?
Tell us what is wrong.
Text version of this sheet
QUICK RULE
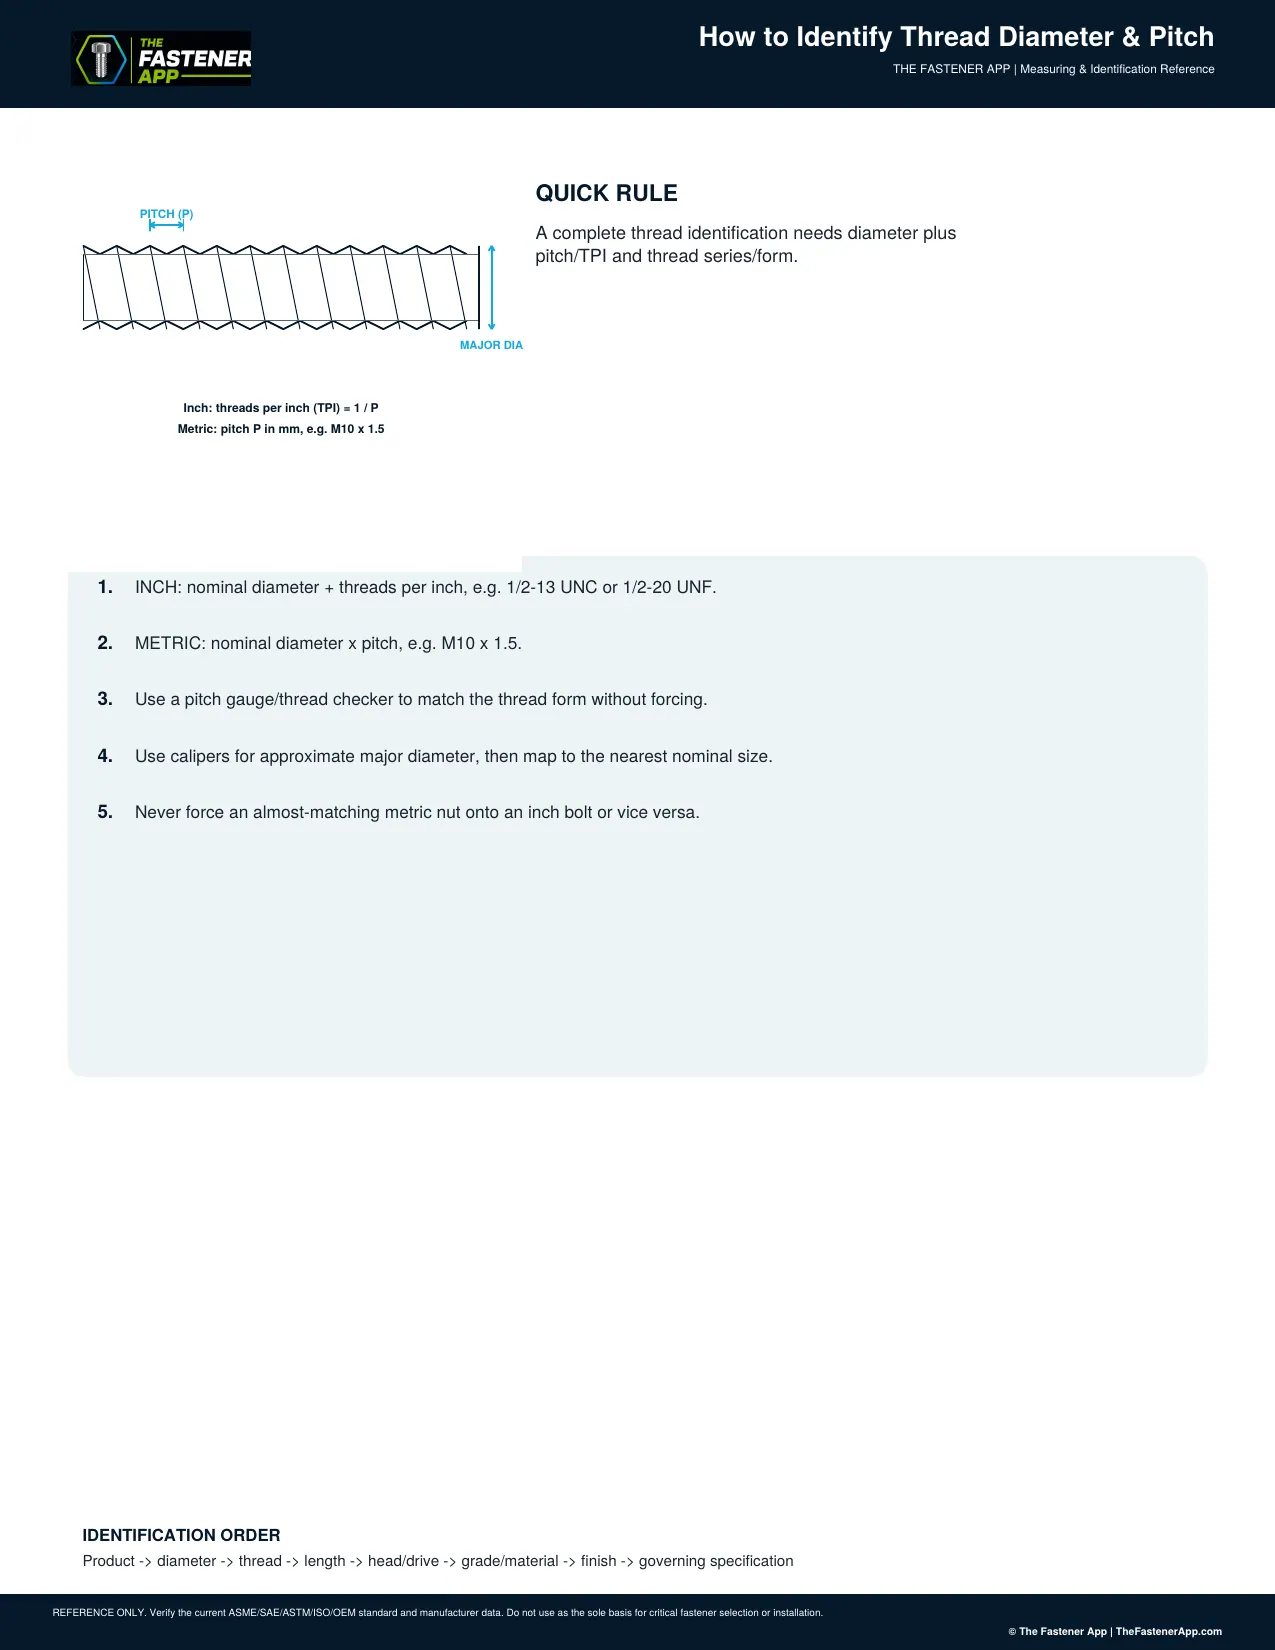
PITCH (P)
A complete thread identification needs diameter plus
pitch/TPI and thread series/form.
MAJOR DIA
Inch: threads per inch (TPI) = 1 / P
Metric: pitch P in mm, e.g. M10 x 1.5
INCH: nominal diameter + threads per inch, e.g. 1/2-13 UNC or 1/2-20 UNF.
METRIC: nominal diameter x pitch, e.g. M10 x 1.5.
Use a pitch gauge/thread checker to match the thread form without forcing.
Use calipers for approximate major diameter, then map to the nearest nominal size.
Never force an almost-matching metric nut onto an inch bolt or vice versa.
IDENTIFICATION ORDER
Product -> diameter -> thread -> length -> head/drive -> grade/material -> finish -> governing specification
REFERENCE ONLY. Verify the current ASME/SAE/ASTM/ISO/OEM standard and manufacturer data. Do not use as the sole basis for critical fastener selection or installation.
Fastener Guide reference FG-CF862F · thefastenerapp.com/fastener-guide/measure-and-identify/how-to-identify-thread-diameter-and-pitch · © The Fastener App. Reference only — verify the current governing standard, drawing and manufacturer data before specifying or installing.